引言
การเชื่อม ซึ่งเป็นรากฐานสำคัญของการผลิตและการก่อสร้างสมัยใหม่ ได้พัฒนาอย่างมีนัยสำคัญตลอดหลายปีที่ผ่านมา จากการเชื่อมอาร์กแบบดั้งเดิมไปจนถึงเทคนิคเลเซอร์ที่ล้ำสมัย สาขานี้ยังคงปรับตัวอย่างต่อเนื่องเพื่อตอบสนองความต้องการที่เพิ่มขึ้นในด้านความแม่นยำ ประสิทธิภาพ และความหลากหลาย บทความนี้ให้การเปรียบเทียบอย่างครอบคลุมระหว่างการเชื่อมเลเซอร์กับวิธีการเชื่อมอื่นๆ โดยมุ่งเน้นที่จุดแข็ง ข้อจำกัด และการประยุกต์ใช้งานในอุตสาหกรรมต่างๆ.
วิทยาศาสตร์เบื้องหลังการเชื่อมเลเซอร์
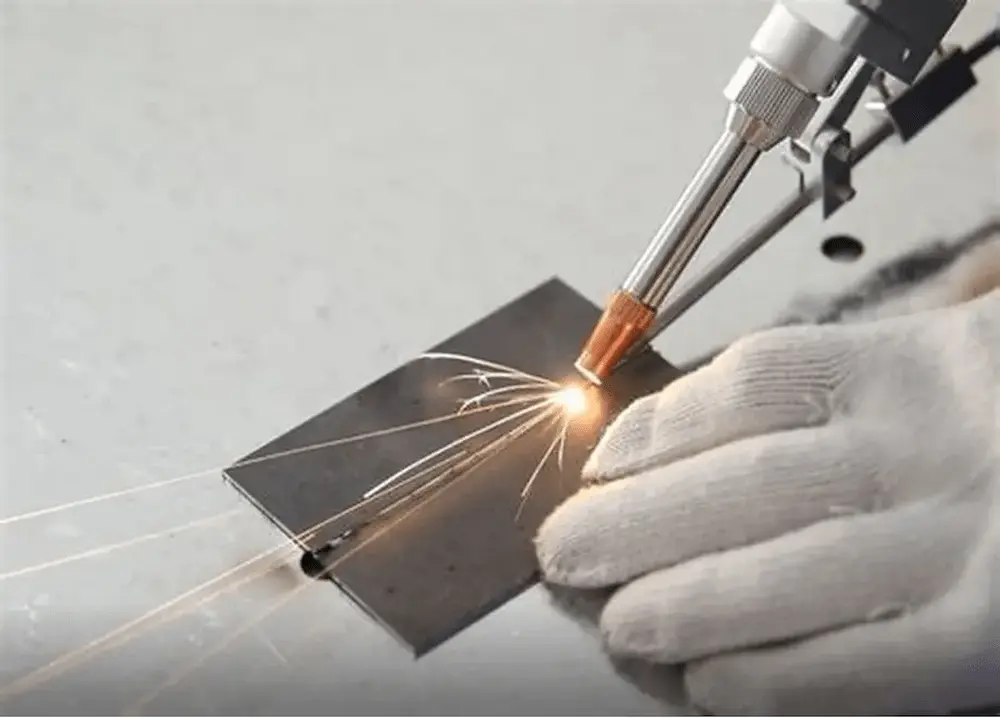
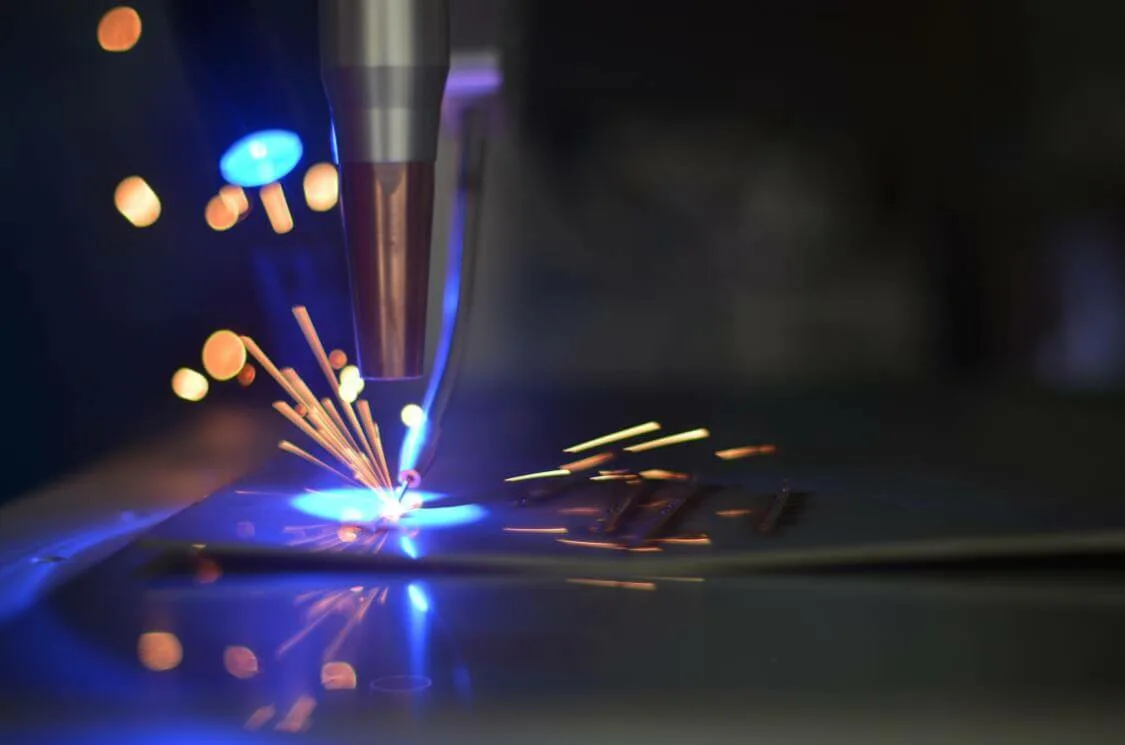
การเชื่อมเลเซอร์ใช้ลำแสงที่มีความเข้มข้นสูงเพื่อหลอมละลายและเชื่อมวัสดุเข้าด้วยกัน กระบวนการนี้มีข้อได้เปรียบเฉพาะหลายประการเหนือวิธีการเชื่อมแบบดั้งเดิม โดยหลักๆ มาจากความแม่นยำและความสามารถในการควบคุมความร้อนที่ป้อนเข้าด้วยความแม่นยำสูง.
หลักการของการเชื่อมเลเซอร์
หลักการพื้นฐานของการเชื่อมเลเซอร์เกี่ยวข้องกับการรวมลำแสงเลเซอร์กำลังสูงไปยังจุดเล็กๆ บนชิ้นงาน พลังงานที่เข้มข้นนี้จะให้ความร้อนแก่วัสดุอย่างรวดเร็วจนถึงจุดหลอมละลาย ทำให้เกิดแอ่งเชื่อม เมื่อเลเซอร์เคลื่อนที่ไปตามเส้นทางการเชื่อมที่ต้องการ วัสดุที่หลอมละลายจะแข็งตัวตามหลัง ทำให้เกิดรอยเชื่อมที่แข็งแรงและแม่นยำ.
ประเด็นสำคัญของกระบวนการเชื่อมเลเซอร์ ได้แก่:
- ความหนาแน่นพลังงานสูง: การเชื่อมเลเซอร์สามารถให้ความหนาแน่นพลังงานสูงมาก ทำให้สามารถเจาะลึกและสร้างรอยเชื่อมที่แคบได้.
- การให้ความร้อนและการเย็นตัวที่รวดเร็ว: กระบวนการนี้เกี่ยวข้องกับการให้ความร้อนอย่างรวดเร็วในพื้นที่ขนาดเล็ก ตามด้วยการเย็นตัวอย่างรวดเร็ว ซึ่งสามารถส่งผลให้เกิดการบิดเบือนน้อยที่สุดและบริเวณที่ได้รับความร้อนน้อย.
- กระบวนการแบบไม่สัมผัส: เนื่องจากลำแสงเลเซอร์ไม่ได้สัมผัสกับชิ้นงานโดยตรง จึงไม่มีการสึกหรอของเครื่องมือ และความเสี่ยงต่อการปนเปื้อนลดลง.
ประเภทของเลเซอร์และการประยุกต์ใช้งาน
เลเซอร์หลายประเภทถูกใช้ในการเชื่อม โดยแต่ละประเภทมีคุณลักษณะและการใช้งานที่เหมาะสมที่สุด:
- เลเซอร์ CO2: เหมาะที่สุดสำหรับการเชื่อมพลาสติก อะคริลิก สิ่งทอ และโลหะบางชนิด.
- เอ็นดี:วายเอจี เลเซอร์: เหมาะสำหรับการเชื่อมโลหะ รวมถึงโลหะสะท้อนแสง.
- ไฟเบอร์เลเซอร์: ยอดเยี่ยมสำหรับการเชื่อมวัสดุบางด้วยความเร็วสูงและการเชื่อมโลหะที่แม่นยำ.
- เลเซอร์ไดโอด: เหมาะสำหรับการเชื่อมพลาสติกและแผ่นโลหะบาง.
บริเวณที่ได้รับความร้อนในการเชื่อมเลเซอร์
บริเวณที่ได้รับความร้อน (HAZ) ในการเชื่อมเลเซอร์โดยทั่วไปมีขนาดเล็กกว่าเมื่อเทียบกับวิธีการเชื่อมแบบดั้งเดิม ส่งผลให้การบิดเบือนจากความร้อนลดลง การเปลี่ยนแปลงคุณสมบัติของวัสดุใกล้รอยเชื่อมน้อยที่สุด และความสามารถในการเชื่อมชิ้นส่วนที่ไวต่อความร้อน.
ข้อดีในการผลิตที่แม่นยำ
การเชื่อมเลเซอร์มีข้อได้เปรียบที่สำคัญหลายประการในการผลิตที่แม่นยำ:
- 高柔性:支持程序化快速切换设计,适合小批量定制生产: รอยเชื่อมสามารถแคบได้ถึง 0.1 มม.
- ความสามารถในการทำซ้ำ: ระบบเลเซอร์ที่ควบคุมด้วยคอมพิวเตอร์รับประกันผลลัพธ์ที่สม่ำเสมอ.
- เหมาะสำหรับระบบอัตโนมัติ: สามารถบูรณาการเข้ากับสายการผลิตอัตโนมัติได้อย่างง่ายดาย.
- 非金属材料:亚克力、木材、塑料、玻璃、复合材料(主要采用CO₂激光器): สามารถเชื่อมวัสดุและความหนาได้หลากหลาย.
- กระบวนการที่สะอาด: มีการกระเด็นน้อยที่สุดและไม่มีการปนเปื้อนจากอิเล็กโทรด.
เทคนิคการเชื่อมแบบดั้งเดิม
แม้ว่าการเชื่อมเลเซอร์จะมีข้อได้เปรียบมากมายในด้านความแม่นยำและความเร็ว แต่เทคนิคการเชื่อมแบบดั้งเดิมยังคงมีบทบาทสำคัญในหลายอุตสาหกรรม เนื่องจากความหลากหลาย ความคุ้มค่า และความเหมาะสมกับวัสดุและเงื่อนไขต่างๆ มาสำรวจวิธีการเชื่อมแบบดั้งเดิมที่พบได้บ่อยที่สุด:
วิธีการเชื่อมอาร์ก
การเชื่อม TIG (ทังสเตนเฉื่อยแก๊ส)
หลักการ: การเชื่อม TIG ใช้อิเล็กโทรดทังสเตนที่ไม่สิ้นเปลืองเพื่อสร้างรอยเชื่อม อาร์กได้รับการปกป้องจากการปนเปื้อนในบรรยากาศด้วยแก๊สปกคลุมเฉื่อย (โดยปกติคืออาร์กอนหรือฮีเลียม).
บริบททางประวัติศาสตร์: ถูกใช้ครั้งแรกในการเชื่อมแมกนีเซียมในอุตสาหกรรมการบินในช่วงสงครามโลกครั้งที่สอง การเชื่อม TIG ได้รับสิทธิบัตรในปี 1942 โดยรัสเซลล์ เมเรดิธ ที่บริษัทนอร์ธรอปแอร์คราฟต์.
อุตสาหกรรมหลัก: การบินและอวกาศ ยานยนต์ นิวเคลียร์ ปิโตรเคมี และการผลิตระดับสูง.
วัสดุที่เหมาะสม: ยอดเยี่ยมสำหรับการเชื่อมชิ้นส่วนบางของสแตนเลส โลหะที่ไม่ใช่เหล็ก เช่น อะลูมิเนียม แมกนีเซียม และโลหะผสมทองแดง โดยเฉพาะอย่างยิ่งมีคุณค่าในความสามารถในการเชื่อมโลหะหายาก เช่น ไทเทเนียม.
พลังงานระยะ: โดยทั่วไป 5-200 แอมป์สำหรับวัสดุบาง และสูงถึง 500 แอมป์สำหรับวัสดุที่หนากว่า.
ความลึกของรอยเชื่อมและความแม่นยำ: สามารถสร้างรอยเชื่อมที่แม่นยำมากได้ บางเพียง 0.1 มม. ความลึกของรอยเชื่อมสามารถอยู่ในช่วงตั้งแต่ผิวเผินไปจนถึงหลายมิลลิเมตร ขึ้นอยู่กับการใช้งานและการตั้งค่ากำลังไฟ.
สถานะปัจจุบัน: การเชื่อม TIG ยังคงเป็นเทคนิคหลัก โดยเฉพาะอย่างยิ่งสำหรับรอยเชื่อมคุณภาพสูงและแม่นยำ ความสามารถในการสร้างรอยเชื่อมที่สะอาดและแข็งแรงบนโลหะหลากหลายชนิดทำให้มั่นใจได้ถึงความเกี่ยวข้องอย่างต่อเนื่องในการผลิตสมัยใหม่.
การเชื่อม MIG (โลหะเฉื่อยแก๊ส)
หลักการ: MIG welding uses a wire electrode that is continuously fed into the weld pool. The arc and weld pool are protected by an external supply of shielding gas.
บริบททางประวัติศาสตร์: Developed in 1948 at the Battelle Memorial Institute, it was initially used for welding aluminum and other non-ferrous materials.
อุตสาหกรรมหลัก: Automotive manufacturing and repair, general fabrication, construction, and shipbuilding.
วัสดุที่เหมาะสม: Widely used for steel, stainless steel, and aluminum. It can be used on materials from thin sheets to thick plates.
พลังงานระยะ: Typically 30-400 amps, with some high-end machines capable of up to 600 amps.
ความลึกของรอยเชื่อมและความแม่นยำ: MIG welding can achieve weld depths from about 1 mm to 13 mm in a single pass, depending on the power and technique used. While not as precise as TIG welding, modern MIG systems can achieve good precision, especially with pulsed power sources.
สถานะปัจจุบัน: MIG welding remains one of the most widely used welding processes in industry due to its speed, versatility, and ease of use. It continues to evolve with advancements in power source technology and wire feed systems.
3. SMAW (Shielded Metal Arc Welding)
หลักการ: SMAW uses a consumable electrode coated in flux to lay the weld. The electrode coating produces gases that protect the weld area from atmospheric contamination.
บริบททางประวัติศาสตร์: Developed in the late 19th century, with significant improvements made in the 1950s in electrode coating technology.
อุตสาหกรรมหลัก: Construction, pipeline welding, shipbuilding, and general repair work.
วัสดุที่เหมาะสม: Can weld most common metals including steel, stainless steel, cast iron, and many alloys. It’s particularly useful for rusty or dirty metals.
พลังงานระยะ: Typically 25-500 amps, depending on the electrode size and material thickness.
ความลึกของรอยเชื่อมและความแม่นยำ: Capable of deep penetration welds, typically from 3 mm to 19 mm in a single pass. Precision is lower compared to TIG or MIG welding due to the nature of the process and slag formation.
สถานะปัจจุบัน: While it has been superseded by more modern techniques in many applications, SMAW remains relevant due to its portability, versatility, and effectiveness in outdoor and rugged conditions. It’s still widely used in construction and field repair work.
4. SAW (Submerged Arc Welding)
หลักการ: The arc burns under a layer of granular flux, which melts to form a protective slag over the weld bead.
บริบททางประวัติศาสตร์: SAW was developed in the 1930s by the National Tube Company in the US, initially for manufacturing large-diameter steel pipes.
อุตสาหกรรมหลัก: Shipbuilding, pressure vessel manufacturing, large steel structures, pipe manufacturing.
วัสดุที่เหมาะสม: Primarily used for carbon steel, low alloy steel, and stainless steel. Typically used for materials 6mm thick and above.
Current Range: 300-2000 amps, with some applications reaching up to 5000 amps.
ความลึกของรอยเชื่อมและความแม่นยำ: Single pass welds can reach 10-20mm deep. Multi-pass welds can join extremely thick plates. Due to full automation, weld quality consistency is high, but it’s not suitable for complex or fine welding work.
สถานะปัจจุบัน: SAW remains a mainstream technology in heavy industries requiring high-efficiency, high-deposition rate welding. With increasing automation, its application range continues to expand.
Gas Welding
หลักการ: Uses combustible gas (usually acetylene) mixed with oxygen to produce a high-temperature flame that melts the base metal and filler material.
บริบททางประวัติศาสตร์: Oxy-acetylene welding was developed in 1903 by French engineers Edmond Fouché and Charles Picard.
อุตสาหกรรมหลัก: Plumbing, automotive repair, small metal product manufacturing, artwork creation.
วัสดุที่เหมาะสม: Suitable for various metals including steel, copper, aluminum, and cast iron. Particularly good for thin sheet materials.
Flame Temperature: Oxy-acetylene welding can reach temperatures of about 3,200°C.
ความลึกของรอยเชื่อมและความแม่นยำ: Typically used for materials under 6mm thick. Precision is relatively low, but skilled operators can achieve quite fine control.
สถานะปัจจุบัน: While largely replaced by other methods in large-scale industrial production, it’s still used in repair work, small-scale production, and specialized applications like jewelry making. Its portability and independence from electricity give it advantages in certain scenarios.
Resistance Welding
หลักการ: Uses heat generated by electrical resistance to melt and join metals.
1. Spot Welding
หลักการ: Applies pressure and current through two electrodes on either side of the workpieces.
บริบททางประวัติศาสตร์: Spot welding technology began in the early 20th century, with Elihu Thomson patenting it in 1925.
อุตสาหกรรมหลัก: Automotive manufacturing, appliance production, aerospace.
วัสดุที่เหมาะสม: Mainly used for thin sheet metals such as low carbon steel, stainless steel, galvanized steel, aluminum alloys.
Current Range: Typically 1,000-20,000 amps, applied for durations from milliseconds to several seconds.
ความลึกของรอยเชื่อมและความแม่นยำ: Weld spot diameters typically range from 3-12mm, with depth depending on material thickness. High precision and good repeatability.
สถานะปัจจุบัน: Spot welding remains a mainstream technology in automated production lines, especially in automotive body assembly.
2. Seam Welding
หลักการ: Similar to spot welding, but uses wheel-shaped electrodes to produce continuous or intermittent seam welds.
บริบททางประวัติศาสตร์: Developed in the early 20th century as an extension of spot welding technology.
อุตสาหกรรมหลัก: Metal container manufacturing, automotive manufacturing, appliance production.
วัสดุที่เหมาะสม: Suitable for most thin sheet metals, including steel, stainless steel, and some non-ferrous metals.
Current Range: Typically 5,000-50,000 amps.
ความลึกของรอยเชื่อมและความแม่นยำ: Can produce continuous sealed seams, typically 3-10mm wide. High precision, particularly suitable for applications requiring gas or liquid-tight seals.
สถานะปัจจุบัน: Seam welding remains the preferred technology in applications requiring long, continuous welds, such as in the manufacture of fuel tanks and food cans.
Specialized Welding Processes
1. Electron Beam Welding (EBW)
หลักการ: Uses a high-velocity electron beam to generate heat for welding. The process is performed in a vacuum.
บริบททางประวัติศาสตร์: EBW technology originated in the 1950s, discovered by German physicist Karl-Heinz Steigerwald while researching electron microscopes.
อุตสาหกรรมหลัก: Aerospace, nuclear industry, automotive (high-end applications), medical device manufacturing.
วัสดุที่เหมาะสม: Can weld almost all metals and some special alloys. Particularly suitable for difficult-to-weld materials like titanium alloys and high-temperature alloys.
พลังงานระยะ: Typically from 1kW to 100kW, with some special applications reaching several hundred kilowatts.
ความลึกของรอยเชื่อมและความแม่นยำ:
- Depth: Can reach 300mm in a single pass, offering the highest penetration capability of all welding methods.
- Precision: Weld width can be as small as 0.5mm, with an extremely small heat-affected zone.
สถานะปัจจุบัน: Remains the preferred technology in high-end applications requiring high depth-to-width ratio and high-quality welds. Its application range is expanding as equipment costs decrease and operation simplifies.
2. Plasma Arc Welding (PAW)
หลักการ: Uses a highly ionized gas (plasma) to produce a high-temperature arc for welding. The plasma arc is more concentrated and stable than a regular arc.
บริบททางประวัติศาสตร์: PAW technology was developed in the late 1950s by Robert Gage as an improvement on TIG welding.
อุตสาหกรรมหลัก: Aerospace, nuclear industry, chemical equipment manufacturing, precision machinery manufacturing.
วัสดุที่เหมาะสม: Suitable for most metals, including stainless steel, nickel-based alloys, titanium alloys. Particularly suitable for welding thin sheets and precision components.
Current Range: Typically 0.1-100 amps, but can reach 300 amps for certain applications.
ความลึกของรอยเชื่อมและความแม่นยำ:
- Depth: Micro-plasma can weld 0.1mm thin sheets, while high-power PAW can reach depths of 10mm.
- Precision: Weld width can be 0.5-5mm, with a small heat-affected zone.
สถานะปัจจุบัน: Widely used in fields requiring high-quality, high-precision welding. Its application is expanding with developments in automation and precise control technology.
3. Friction Welding
หลักการ: Uses heat generated by friction to soften the metal at the contact surface, then joins under pressure. No filler material or shielding gas is required.
บริบททางประวัติศาสตร์: The concept of friction welding was first proposed in the 19th century, but practical applications didn’t begin until the 1950s.
อุตสาหกรรมหลัก: Automotive, aerospace, oil and gas industry.
วัสดุที่เหมาะสม: Can weld a variety of similar or dissimilar metals, including steel, aluminum, copper, nickel-based alloys. Particularly suitable for joining cylindrical parts.
พลังงานระยะ: Depends on workpiece size and material, can range from a few kilowatts to several hundred kilowatts.
ความลึกของรอยเชื่อมและความแม่นยำ:
- Depth: Theoretically unlimited, in practice can weld solid shafts up to 250mm in diameter.
- Precision: High joint quality, no porosity or inclusions.
สถานะปัจจุบัน: Remains the preferred technology in specific applications (such as drive shaft and turbine blade connections). With the emergence of new variants (like friction stir welding), its application range is continually expanding.
Comparison of Welding Techniques
To provide a comprehensive overview of the different welding techniques, let’s refer to the following comparison table:
| Characteristic | 激光焊接 | Electron Beam Welding (EBW) | TIG Welding (GTAW) | MIG Welding (GMAW) | Submerged Arc Welding (SAW) | Friction Welding |
|---|---|---|---|---|---|---|
| Welding Precision | Very High (0.1mm) | Extremely High (0.5mm) | สูง | ปานกลาง | ปานกลาง | สูง |
| Thickness Range | 0.01mm – 10mm+ | Up to 300mm | 0.1mm – 6mm | 0.6mm – 50mm+ | 6mm – 40mm+ | 1mm – 100mm+ |
| วัสดุที่เหมาะสม | Almost all metals, special alloys | All metals, reactive metals | Most metals, stainless steel, aluminum, titanium | Steel, stainless steel, aluminum | Carbon steel, low alloy steel | Most metals, dissimilar metals |
| Welding Speed | High (up to 10m/min) | สูง | Low (0.1-0.5m/min) | Moderate (1-2m/min) | High (0.5-5m/min) | ปานกลาง |
| Heat Affected Zone | Very Small | Extremely Small | Small | ปานกลาง | Large | Small |
| ต้นทุนอุปกรณ์ | สูง | Very High | Low to Moderate | ปานกลาง | Moderate to High | Moderate to High |
| Operating Cost | Low | High (vacuum required) | ปานกลาง | Low to Moderate | Moderate (flux cost) | Low |
| Automation Potential | Very High | Very High | ปานกลาง | สูง | Very High | สูง |
| ผลกระทบต่อสิ่งแวดล้อม | Low (some fumes) | Very Low (vacuum) | Moderate (shielding gas) | Moderate (fumes) | Low (flux covers arc) | Very Low (no fumes) |
| Worker Skill Required | ปานกลาง | สูง | Very High | ปานกลาง | Low | Low |
| Joint Fit-up Requirement | Very Strict | Very Strict | ปานกลาง | Flexible | ปานกลาง | Strict |
| Power Source | Laser | Electron Beam | Electric Arc | Electric Arc | Electric Arc | Mechanical Friction |
| Shielding | Gas or None | Vacuum | Inert Gas | Gas | Flux | None |
| Filler Material | ไม่บังคับ | Usually None | ไม่บังคับ | Required | Required | None |
| Distortion | Very Low | Very Low | Low | ปานกลาง | สูง | Low |
| การใช้งานทั่วไป | Automotive, electronics, medical devices | Aerospace, nuclear industry | Aerospace, chemical industry | General fabrication, automotive | Shipbuilding, large pipes | Automotive, oil & gas industry |
Note: The values and ranges provided are general and may vary depending on specific equipment, materials, and applications.
สรุป
In conclusion, while each welding technique has its place in modern manufacturing, laser welding stands out in several key areas:
- Precision and Speed: With an unparalleled precision of 0.1mm and welding speeds up to 10m/min, laser welding is ideal for industries requiring high-quality, fast production such as automotive and electronics.
- Minimal Heat Affected Zone: This reduces material distortion, crucial for working with sensitive components and maintaining the integrity of the welded materials.
- Automation Potential: Laser welding’s high compatibility with automated systems makes it well-suited for modern, high-volume production environments.
- ความอเนกประสงค์ของวัสดุ: The ability to work with a wide range of materials, including traditionally difficult-to-weld alloys, expands its applicability across various industries.
- Future Relevance: As industries continue to demand higher precision, faster production speeds, and the ability to work with advanced materials, laser welding is positioned to play an increasingly important role.
However, it’s important to note that traditional welding methods will continue to be valuable in many applications. The choice of welding technique should always be based on specific project requirements, material considerations, and economic factors. As manufacturing evolves, a thorough understanding of all available welding technologies will remain crucial for making informed decisions in production processes.