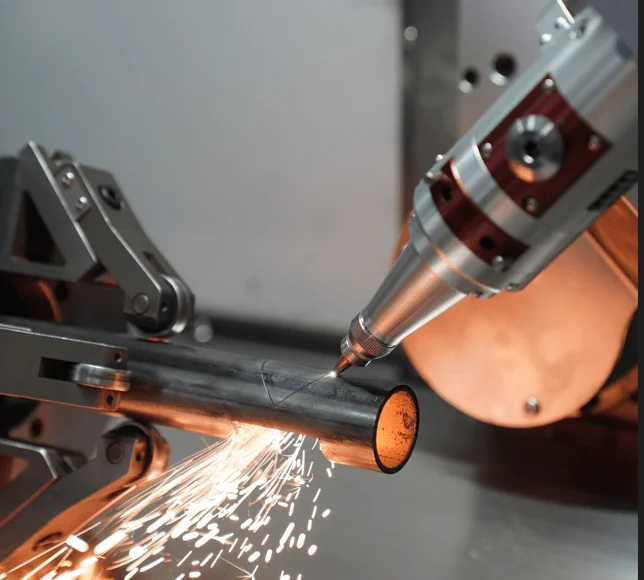
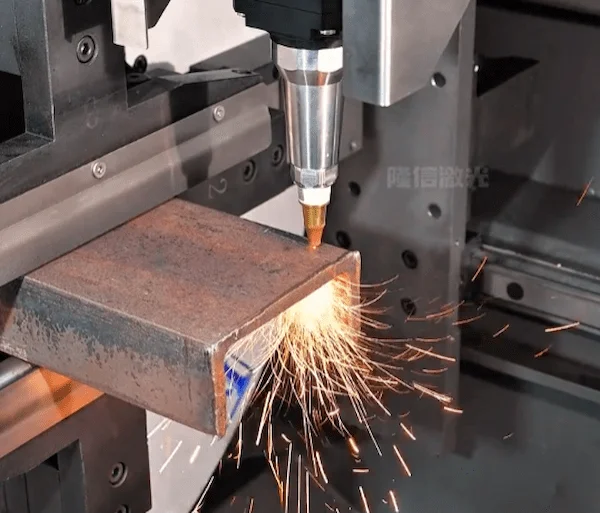
มีหลายปัจจัยที่ส่งผลต่อความแม่นยำในการตัดของ เครื่องตัดท่อเลเซอร์- โดยเฉพาะอย่างยิ่ง มีเหตุผลหลักดังต่อไปนี้:
1.รูปร่างของลำแสงเลเซอร์
ลำแสงจากเลเซอร์จะเรียว ดังนั้นรอยกรีดที่ตัดออกก็จะเรียวด้วย ในกรณีนี้ ความหนาของการตัดเหล็กสแตนเลส 0.6 มม. จะเล็กกว่ารอยสลิต 3 มม. ดังนั้นรูปร่างของความเร็วแสงเลเซอร์จะเป็นปัจจัยสำคัญที่ส่งผลต่อความแม่นยำในการตัดของเครื่องตัดท่อด้วยเลเซอร์ท่อโลหะ ในสภาพแสงความเร็วเลเซอร์รูปทรงกรวยนี้ ยิ่งความหนาของชิ้นงานมากเท่าใด ความแม่นยำก็จะยิ่งต่ำลงเท่านั้น
2.ขนาดจุดของลำแสงเลเซอร์
ขนาดสปอตยังเป็นปัจจัยหนึ่งที่ส่งผลต่อความแม่นยำในการตัดของเครื่องตัดเลเซอร์แบบท่อ เมื่อเลเซอร์รูปทรงกรวยโฟกัสเข้าหากัน จุดจะเล็กลงเรื่อยๆ ความแม่นยำในการตัดด้วยเลเซอร์ก็จะสูงขึ้นตามไปด้วย จุดที่เล็กที่สุดสามารถมีได้ถึง 0.01 มม. สามารถตัดช่องว่างการตัดเล็ก ๆ ออกได้เพื่อให้มั่นใจในความแม่นยำในการประมวลผล
3.วัสดุต่างๆของท่อ
Different materials pipe laser cutting machine cutting accuracy is also less different, even the same material, if the composition of the material is different, the cutting accuracy will also be different. Therefore, the workpiece material on the pipe laser cutting accuracy also has a certain impact. For example, under the same circumstances, stainless steel has higher cutting accuracy and smoother cutting surface than aluminum.
Generally speaking, different pipes to be cut have different physical and chemical properties.
In terms of physical properties, the pipes to be cut vary in terms of hardness, melting and boiling points, and whether they are easy to melt. In terms of chemical properties, such as the flammability, stability, oxidation, and combustion-supporting properties of the pipes to be cut, there are also great differences. This makes the different pipes to be cut different in terms of the size of the chuck, the type and pressure of the auxiliary gas. And the requirements such as laser cutting power are different.
Under normal circumstances, the greater the thickness of the pipe to be cut, the higher the laser cutting power required. When cutting pipes of special materials such as aluminum pipes, copper pipes, stainless steel pipes, and even pipes made of materials with excellent oxidation resistance, as well as pipes of special shapes such as special-shaped pipes, H-shaped steel, channel steel, and angle steel, the laser The cutting power, the choice of auxiliary gas type, and the performance of the chuck itself also have different requirements. When cutting and processing lengthened and weighted pipe fittings, in addition to considering laser power and auxiliary gas, the selection of supporting components must also be considered to ensure the accuracy of the entire cutting process.
4.ความหนาของชิ้นงาน
ยิ่งความหนาของชิ้นงานมากเท่าใด ความแม่นยำก็จะยิ่งต่ำลงและรอยสลิตก็จะมากขึ้นเท่านั้น เนื่องจากลำแสงเลเซอร์มีรูปทรงกรวย แผ่นสลิทตัดจึงมีรูปทรงกรวยด้วย ตัวอย่างเช่น ช่องว่างการตัดของวัสดุที่มีความหนา 0.3 มม. จะน้อยกว่าวัสดุที่มีความหนา 2 มม. มาก
5.เลือกระบบตัดได้
For hardware to fully play its role, suitable software assistance is needed, such as an excellent pipe cutting system. The more popular pipe cutting systems on the market now include cutting systems independently developed by FS, Siemens, Beckhoff or companies. Different systems support different cutting methods, pipe shapes, and number of chucks. For example, FSCUT’s system supports offset tube center error in production to improve through holes cutting precision. Excellent tube cutting software is one of the necessary factors to achieve high precision.
6.การเลือกก๊าซเสริม
When the laser cutting machine is working, the light spot formed by focusing the laser beam through the lens is irradiated on the surface of the material to be cut, causing the temperature to rise in a very short time, thereby reaching the melting point or boiling point of the material to be cut. During the cutting process, the surface of the material to be cut can reflect the laser to a certain extent. During cutting, auxiliary gas can be blown to increase the absorption of the laser by the surface of the material to be cut and improve cutting efficiency. Auxiliary gases generally use oxygen, nitrogen, compressed air and other inert gases.
Oxygen is commonly used as an auxiliary gas because oxygen promotes the oxidation reaction on the surface of the pipe being cut, thereby improving cutting efficiency. When the laser cutting power and cutting speed are constant, the greater the oxygen pressure, the larger the cutting seam, and the cutting section stripes will be thicker and larger; when the oxygen pressure is reduced, the cutting seam becomes thinner, and the cutting section stripes are thin and smooth, but when When the pressure drops to a certain value, the cutting effect on one side of the pipe will be significant, but at the same time, slag will appear. The slag falling to the opposite side will affect the entire cutting accuracy, and sometimes it will even be difficult to cut off the cut pipe.
When cutting high-thickness pipes, special-shaped pipes or pipes of special materials, nitrogen and other inert gases need to be used as auxiliary gases. Combined with the metal and physical properties of the pipe being cut, compressed air can be selected as the auxiliary gas in order to control costs without affecting the overall cutting efficiency.
7.สรุป
โดยทั่วไป ปัจจัยที่ส่งผลต่อความแม่นยำในการตัดท่อมีความซับซ้อน ดังนั้นผู้ซื้อควรเลือกผู้ผลิตเครื่องตัดท่อเลเซอร์ที่มีคุณภาพเชื่อถือได้และประสบการณ์ที่เป็นผู้ใหญ่ และแสดงความต้องการของตนอย่างแข็งขันและให้ข้อมูลโดยละเอียดในระหว่างกระบวนการจัดซื้อ การเลือกอุปกรณ์ฮาร์ดแวร์ที่ดีเท่านั้นจึงจะรับประกันความเสถียรของความแม่นยำในการตัดได้