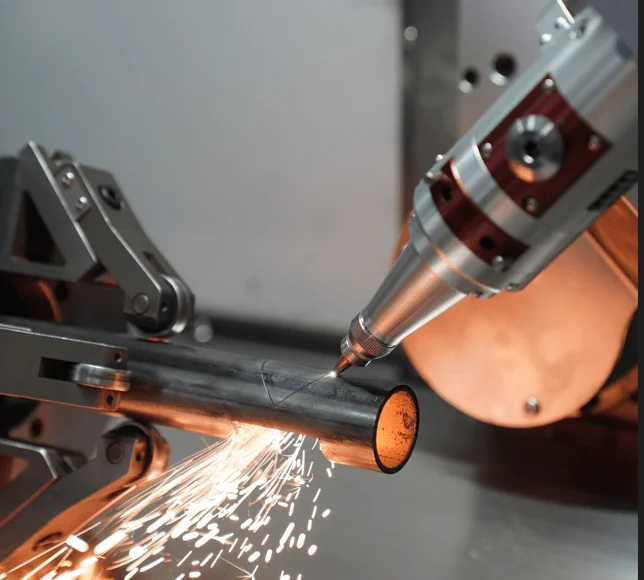
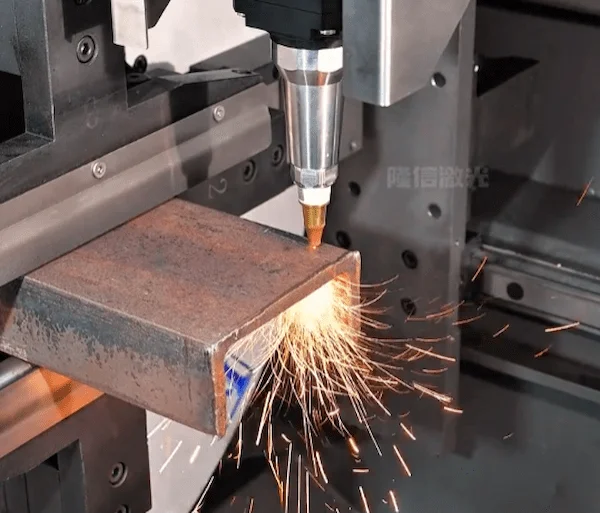
Kesim hassasiyetini etkileyen birçok faktör vardır lazer boru kesme makinası. Spesifik olarak, aşağıdaki ana nedenler söz konusudur:
1.Lazer ışınının şekli
Lazerden gelen ışın koniktir, bu nedenle kesilen yarık da koniktir, bu durumda 0,6MM paslanmaz çeliğin kesme kalınlığı 3MM yarıktan daha küçük olacaktır. Bu nedenle, lazer ışık hızının şekli, metal boru lazer boru kesme makinesinin kesme doğruluğunu etkileyen önemli bir faktör olacaktır. Bu koni şeklindeki lazer ışık hızı koşullarında, iş parçasının kalınlığı ne kadar büyük olursa, doğruluk o kadar düşük olacaktır.
2. Lazer ışınının spot boyutu
Spot boyutu da boru lazer kesim makinesinin kesim hassasiyetini etkileyen faktörlerden biridir. Koni şeklindeki lazer birlikte odaklandığında, nokta küçülür ve küçülür, lazer kesim doğruluğu o kadar yüksek olur. En küçük nokta 0,01 mm'ye kadar olabilir, işleme doğruluğunu sağlamak için küçük kesme boşluğunu kesebilir.
3. Borunun farklı malzemeleri
Different materials pipe laser cutting machine cutting accuracy is also less different, even the same material, if the composition of the material is different, the cutting accuracy will also be different. Therefore, the workpiece material on the pipe laser cutting accuracy also has a certain impact. For example, under the same circumstances, stainless steel has higher cutting accuracy and smoother cutting surface than aluminum.
Generally speaking, different pipes to be cut have different physical and chemical properties.
In terms of physical properties, the pipes to be cut vary in terms of hardness, melting and boiling points, and whether they are easy to melt. In terms of chemical properties, such as the flammability, stability, oxidation, and combustion-supporting properties of the pipes to be cut, there are also great differences. This makes the different pipes to be cut different in terms of the size of the chuck, the type and pressure of the auxiliary gas. And the requirements such as laser cutting power are different.
Under normal circumstances, the greater the thickness of the pipe to be cut, the higher the laser cutting power required. When cutting pipes of special materials such as aluminum pipes, copper pipes, stainless steel pipes, and even pipes made of materials with excellent oxidation resistance, as well as pipes of special shapes such as special-shaped pipes, H-shaped steel, channel steel, and angle steel, the laser The cutting power, the choice of auxiliary gas type, and the performance of the chuck itself also have different requirements. When cutting and processing lengthened and weighted pipe fittings, in addition to considering laser power and auxiliary gas, the selection of supporting components must also be considered to ensure the accuracy of the entire cutting process.
4. İş parçası kalınlığı
İş parçasının kalınlığı ne kadar büyükse, hassasiyet o kadar düşük ve yarık o kadar büyük olur. Lazer ışını konik olduğundan, kesme yarığı da koniktir. Örneğin, 0,3 mm kalınlığındaki bir malzemenin kesme boşluğu, 2 mm kalınlığındaki bir malzemeden çok daha küçüktür.
5. Kesme sistemi seçimi
For hardware to fully play its role, suitable software assistance is needed, such as an excellent pipe cutting system. The more popular pipe cutting systems on the market now include cutting systems independently developed by FS, Siemens, Beckhoff or companies. Different systems support different cutting methods, pipe shapes, and number of chucks. For example, FSCUT’s system supports offset tube center error in production to improve through holes cutting precision. Excellent tube cutting software is one of the necessary factors to achieve high precision.
6. Yardımcı gaz seçimi
When the laser cutting machine is working, the light spot formed by focusing the laser beam through the lens is irradiated on the surface of the material to be cut, causing the temperature to rise in a very short time, thereby reaching the melting point or boiling point of the material to be cut. During the cutting process, the surface of the material to be cut can reflect the laser to a certain extent. During cutting, auxiliary gas can be blown to increase the absorption of the laser by the surface of the material to be cut and improve cutting efficiency. Auxiliary gases generally use oxygen, nitrogen, compressed air and other inert gases.
Oxygen is commonly used as an auxiliary gas because oxygen promotes the oxidation reaction on the surface of the pipe being cut, thereby improving cutting efficiency. When the laser cutting power and cutting speed are constant, the greater the oxygen pressure, the larger the cutting seam, and the cutting section stripes will be thicker and larger; when the oxygen pressure is reduced, the cutting seam becomes thinner, and the cutting section stripes are thin and smooth, but when When the pressure drops to a certain value, the cutting effect on one side of the pipe will be significant, but at the same time, slag will appear. The slag falling to the opposite side will affect the entire cutting accuracy, and sometimes it will even be difficult to cut off the cut pipe.
When cutting high-thickness pipes, special-shaped pipes or pipes of special materials, nitrogen and other inert gases need to be used as auxiliary gases. Combined with the metal and physical properties of the pipe being cut, compressed air can be selected as the auxiliary gas in order to control costs without affecting the overall cutting efficiency.
7.Özet
Genel olarak, boru kesme hassasiyetini etkileyen faktörler karmaşıktır. Bu nedenle, alıcılar güvenilir kalite ve olgun deneyime sahip lazer boru kesme makinesi üreticilerini seçmeli ve tedarik sürecinde ihtiyaçlarını aktif olarak ifade etmeli ve ayrıntılı bilgi sağlamalıdır. Yalnızca iyi donanım ekipmanı seçilerek kesim doğruluğunun istikrarı sağlanabilir.