Hay muchos factores que afectan la precisión de corte de máquina cortadora de tubos por láser. En concreto, existen las siguientes razones principales:
1.La forma del rayo láser.
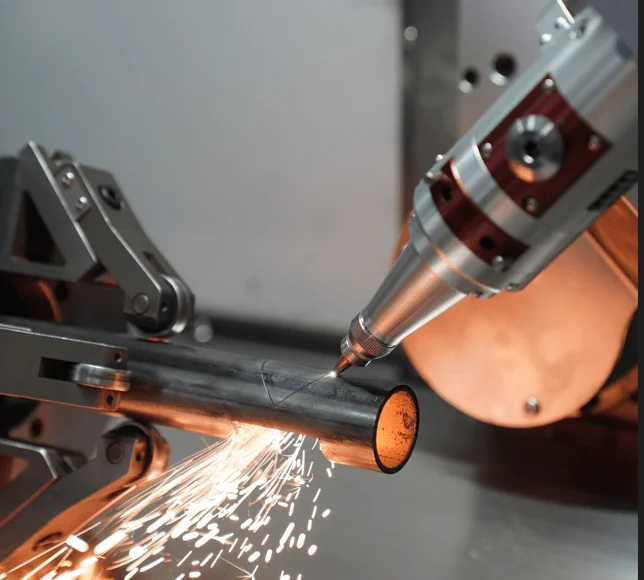
El haz del láser es cónico, por lo que la hendidura cortada también es cónica; en este caso, el espesor de corte del acero inoxidable de 0,6 mm será menor que el de la hendidura de 3 mm. Por lo tanto, la forma de la velocidad de la luz láser será un factor importante que afectará la precisión de corte de la máquina cortadora de tubos láser para tubos metálicos. En estas condiciones de velocidad de luz del láser en forma de cono, cuanto mayor sea el espesor de la pieza de trabajo, menor será la precisión.
2.El tamaño del punto del rayo láser.
El tamaño del punto también es uno de los factores que afectan la precisión de corte de la máquina cortadora láser de tubos. Cuando el láser en forma de cono se enfoca juntos, el punto se volverá cada vez más pequeño, mayor será la precisión del corte por láser. El punto más pequeño puede ser de hasta 0,01 mm y puede cortar el pequeño espacio de corte para garantizar la precisión del procesamiento.
3.Los diferentes materiales de la tubería.
Different materials pipe laser cutting machine cutting accuracy is also less different, even the same material, if the composition of the material is different, the cutting accuracy will also be different. Therefore, the workpiece material on the pipe laser cutting accuracy also has a certain impact. For example, under the same circumstances, stainless steel has higher cutting accuracy and smoother cutting surface than aluminum.
Generally speaking, different pipes to be cut have different physical and chemical properties.
In terms of physical properties, the pipes to be cut vary in terms of hardness, melting and boiling points, and whether they are easy to melt. In terms of chemical properties, such as the flammability, stability, oxidation, and combustion-supporting properties of the pipes to be cut, there are also great differences. This makes the different pipes to be cut different in terms of the size of the chuck, the type and pressure of the auxiliary gas. And the requirements such as laser cutting power are different.
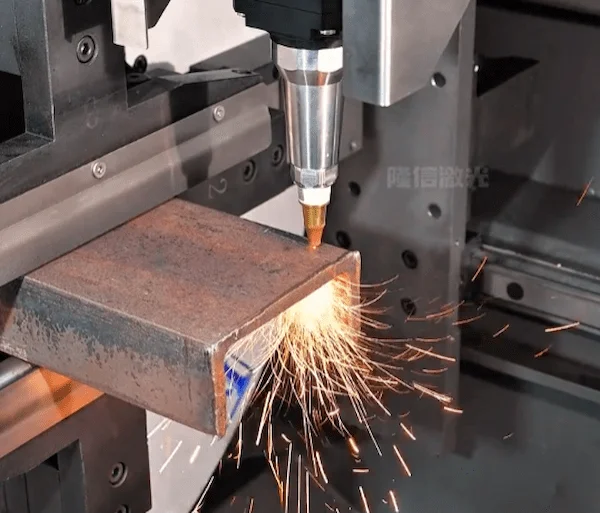
Under normal circumstances, the greater the thickness of the pipe to be cut, the higher the laser cutting power required. When cutting pipes of special materials such as aluminum pipes, copper pipes, stainless steel pipes, and even pipes made of materials with excellent oxidation resistance, as well as pipes of special shapes such as special-shaped pipes, H-shaped steel, channel steel, and angle steel, the laser The cutting power, the choice of auxiliary gas type, and the performance of the chuck itself also have different requirements. When cutting and processing lengthened and weighted pipe fittings, in addition to considering laser power and auxiliary gas, the selection of supporting components must also be considered to ensure the accuracy of the entire cutting process.
4.Espesor de la pieza de trabajo
Cuanto mayor sea el espesor de la pieza de trabajo, menor será la precisión y mayor será la hendidura. Puesto que el rayo láser es cónico, la ranura de corte también es cónica. Por ejemplo, el espacio de corte de un material con un espesor de 0,3 mm es mucho más pequeño que el de un material con un espesor de 2 mm.
5.Elección del sistema de corte
For hardware to fully play its role, suitable software assistance is needed, such as an excellent pipe cutting system. The more popular pipe cutting systems on the market now include cutting systems independently developed by FS, Siemens, Beckhoff or companies. Different systems support different cutting methods, pipe shapes, and number of chucks. For example, FSCUT’s system supports offset tube center error in production to improve through holes cutting precision. Excellent tube cutting software is one of the necessary factors to achieve high precision.
6.Selección de gas auxiliar.
When the laser cutting machine is working, the light spot formed by focusing the laser beam through the lens is irradiated on the surface of the material to be cut, causing the temperature to rise in a very short time, thereby reaching the melting point or boiling point of the material to be cut. During the cutting process, the surface of the material to be cut can reflect the laser to a certain extent. During cutting, auxiliary gas can be blown to increase the absorption of the laser by the surface of the material to be cut and improve cutting efficiency. Auxiliary gases generally use oxygen, nitrogen, compressed air and other inert gases.
Oxygen is commonly used as an auxiliary gas because oxygen promotes the oxidation reaction on the surface of the pipe being cut, thereby improving cutting efficiency. When the laser cutting power and cutting speed are constant, the greater the oxygen pressure, the larger the cutting seam, and the cutting section stripes will be thicker and larger; when the oxygen pressure is reduced, the cutting seam becomes thinner, and the cutting section stripes are thin and smooth, but when When the pressure drops to a certain value, the cutting effect on one side of the pipe will be significant, but at the same time, slag will appear. The slag falling to the opposite side will affect the entire cutting accuracy, and sometimes it will even be difficult to cut off the cut pipe.
When cutting high-thickness pipes, special-shaped pipes or pipes of special materials, nitrogen and other inert gases need to be used as auxiliary gases. Combined with the metal and physical properties of the pipe being cut, compressed air can be selected as the auxiliary gas in order to control costs without affecting the overall cutting efficiency.
7.Resumen
En general, los factores que afectan la precisión del corte de tuberías son complejos. Por lo tanto, los compradores deben elegir fabricantes de máquinas cortadoras de tubos por láser con calidad confiable y experiencia madura, y expresar activamente sus necesidades y proporcionar información detallada durante el proceso de adquisición. Sólo seleccionando un buen equipo de hardware se puede garantizar la estabilidad de la precisión del corte.