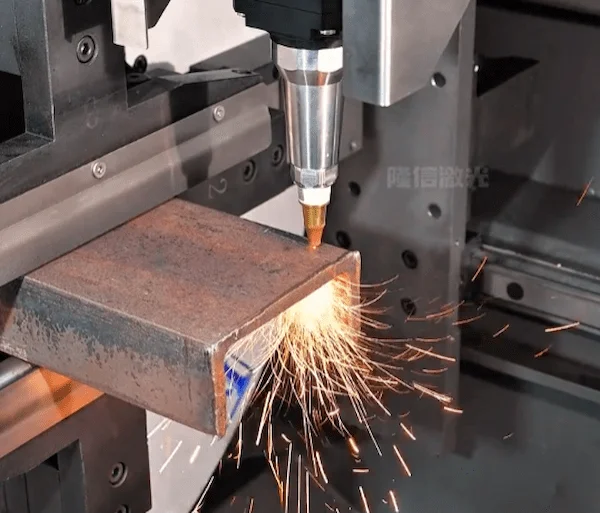
Có nhiều yếu tố ảnh hưởng đến độ chính xác cắt của máy cắt ống laser. Cụ thể có những nguyên nhân chính sau:
1.Hình dạng của chùm tia laser
Chùm tia laser được làm thon dần nên khe cắt ra cũng thon dần, trong trường hợp này độ dày cắt inox 0,6MM sẽ nhỏ hơn khe 3MM. Do đó, hình dạng của tốc độ ánh sáng laser sẽ là yếu tố chính ảnh hưởng đến độ chính xác cắt của máy cắt ống laser ống kim loại. Ở tốc độ laser hình nón này trong điều kiện ánh sáng, độ dày của phôi càng lớn thì độ chính xác sẽ càng thấp.
2. Kích thước điểm của chùm tia laser
Kích thước điểm cũng là một trong những yếu tố ảnh hưởng đến độ chính xác cắt của máy cắt laser ống. Khi các tia laser hình nón tập trung lại với nhau, điểm sẽ ngày càng nhỏ hơn, độ chính xác cắt laser càng cao. Điểm nhỏ nhất có thể lên tới 0,01mm, có thể cắt bỏ khoảng cách cắt nhỏ để đảm bảo độ chính xác khi xử lý.
3. Các vật liệu khác nhau của đường ống
Different materials pipe laser cutting machine cutting accuracy is also less different, even the same material, if the composition of the material is different, the cutting accuracy will also be different. Therefore, the workpiece material on the pipe laser cutting accuracy also has a certain impact. For example, under the same circumstances, stainless steel has higher cutting accuracy and smoother cutting surface than aluminum.
Generally speaking, different pipes to be cut have different physical and chemical properties.
In terms of physical properties, the pipes to be cut vary in terms of hardness, melting and boiling points, and whether they are easy to melt. In terms of chemical properties, such as the flammability, stability, oxidation, and combustion-supporting properties of the pipes to be cut, there are also great differences. This makes the different pipes to be cut different in terms of the size of the chuck, the type and pressure of the auxiliary gas. And the requirements such as laser cutting power are different.
Under normal circumstances, the greater the thickness of the pipe to be cut, the higher the laser cutting power required. When cutting pipes of special materials such as aluminum pipes, copper pipes, stainless steel pipes, and even pipes made of materials with excellent oxidation resistance, as well as pipes of special shapes such as special-shaped pipes, H-shaped steel, channel steel, and angle steel, the laser The cutting power, the choice of auxiliary gas type, and the performance of the chuck itself also have different requirements. When cutting and processing lengthened and weighted pipe fittings, in addition to considering laser power and auxiliary gas, the selection of supporting components must also be considered to ensure the accuracy of the entire cutting process.
4. Độ dày phôi
Độ dày của phôi càng lớn thì độ chính xác càng thấp và khe càng lớn. Vì chùm tia laser có dạng hình nón nên khe cắt cũng có dạng hình nón. Ví dụ, khoảng cách cắt của vật liệu có độ dày 0,3 mm nhỏ hơn nhiều so với vật liệu có độ dày 2 mm.
5. Lựa chọn hệ thống cắt
For hardware to fully play its role, suitable software assistance is needed, such as an excellent pipe cutting system. The more popular pipe cutting systems on the market now include cutting systems independently developed by FS, Siemens, Beckhoff or companies. Different systems support different cutting methods, pipe shapes, and number of chucks. For example, FSCUT’s system supports offset tube center error in production to improve through holes cutting precision. Excellent tube cutting software is one of the necessary factors to achieve high precision.
6. Lựa chọn khí phụ trợ
When the laser cutting machine is working, the light spot formed by focusing the laser beam through the lens is irradiated on the surface of the material to be cut, causing the temperature to rise in a very short time, thereby reaching the melting point or boiling point of the material to be cut. During the cutting process, the surface of the material to be cut can reflect the laser to a certain extent. During cutting, auxiliary gas can be blown to increase the absorption of the laser by the surface of the material to be cut and improve cutting efficiency. Auxiliary gases generally use oxygen, nitrogen, compressed air and other inert gases.
Oxygen is commonly used as an auxiliary gas because oxygen promotes the oxidation reaction on the surface of the pipe being cut, thereby improving cutting efficiency. When the laser cutting power and cutting speed are constant, the greater the oxygen pressure, the larger the cutting seam, and the cutting section stripes will be thicker and larger; when the oxygen pressure is reduced, the cutting seam becomes thinner, and the cutting section stripes are thin and smooth, but when When the pressure drops to a certain value, the cutting effect on one side of the pipe will be significant, but at the same time, slag will appear. The slag falling to the opposite side will affect the entire cutting accuracy, and sometimes it will even be difficult to cut off the cut pipe.
When cutting high-thickness pipes, special-shaped pipes or pipes of special materials, nitrogen and other inert gases need to be used as auxiliary gases. Combined with the metal and physical properties of the pipe being cut, compressed air can be selected as the auxiliary gas in order to control costs without affecting the overall cutting efficiency.
7.Tóm tắt
Nhìn chung, các yếu tố ảnh hưởng đến độ chính xác của việc cắt ống rất phức tạp. Vì vậy, người mua nên chọn những nhà sản xuất máy cắt ống laser có chất lượng đáng tin cậy và kinh nghiệm chín chắn, đồng thời tích cực bày tỏ nhu cầu của mình và cung cấp thông tin chi tiết trong quá trình mua sắm. Chỉ bằng cách lựa chọn thiết bị phần cứng tốt, độ ổn định của độ chính xác cắt mới có thể được đảm bảo.