1. レーザー切断機のフライングカット機能の紹介
フライングカットは、フライング切断またはスキャン切断とも呼ばれ、円形または円形の内穴を持つ部品を切断する過程で、レーザーヘッドが持ち上げずに一方の部品から次の部品へ移動する切断方法を指します。このアプローチにより、切断効率が大幅に向上します。.
パイプ材料の穴が規則的な形状(円形、長方形など)で、一定の規則的なパターンで配置されている場合、フライングカットは同じ方向のセグメントを接続して連続切断を行うことができ、切断速度が大幅に向上し、加工時間を節約します。.
この技術は、その高効率と精度の特性により、金属加工、自動車製造、電子機器など多くの分野で広く応用されています。.
2. レーザーフライングカット技術の原理
フライングカット技術は、レーザービームの動きを迅速かつ正確に制御できる高精度のレーザー切断装置に依存しています。この高度な技術は、従来の順次切断方法からインテリジェントな経路最適化への根本的な転換を表しています。.
(1)フライングカットの核心メカニズム
経路最適化戦略
フライングカットは、その核心において、レーザーヘッドが効率的なグリッドパターンで移動できるようにする高度な経路最適化アルゴリズムを利用します。1つの切断を完了してから次の切断に移る代わりに、システムは水平および垂直の切断ラインを実行しながら、特定のエッジでレーザーを戦略的にオン/オフします。このアプローチにより、複数の切断を同時に処理でき、全体のサイクルタイムを大幅に短縮します。.
スマートな方向転換
レーザーヘッドが方向を変えるとき、鋭い角のターンではなく接線半径遷移を採用します。この技術には2つの目的があります:
- 遷移を通じて最適な切断速度を維持することで切断時間を短縮
- 機器部品の機械的摩耗を最小限に抑え、機械の寿命を延長
レーザー制御の精度
システムはレーザー起動タイミングを正確に制御し、正確な瞬間にビームをオン/オフしてクリーンな切断を確保しながら、不要なレーザー動作時間を最小限に抑えます。この選択的起動は、エネルギー効率と切断品質の向上の両方に貢献します。.
(2)従来方法に対する利点
従来のアプローチの限界:従来のレーザー切断は、レーザーヘッドが次のタスクに移動する前に各個別の切断を完了しなければならない単一経路方式に従います。この順次アプローチは信頼性がありますが、複数の繰り返しパターンを含むプロジェクトでは本質的に時間がかかります。.
3. レーザーフライングカット機能のさまざまなタイプ
(1)アークフライングカット
規則的に配置された 円形穴, の場合、丸パイプでも角パイプでも、, アークフライングカット を使用する必要があります。.
円間のフライング接続の最大距離: 円形穴間の開始点距離が設定パラメータより小さい場合、フライングカットラインを生成できます。このパラメータは円形穴間の距離よりわずかに大きく設定することをお勧めします。.
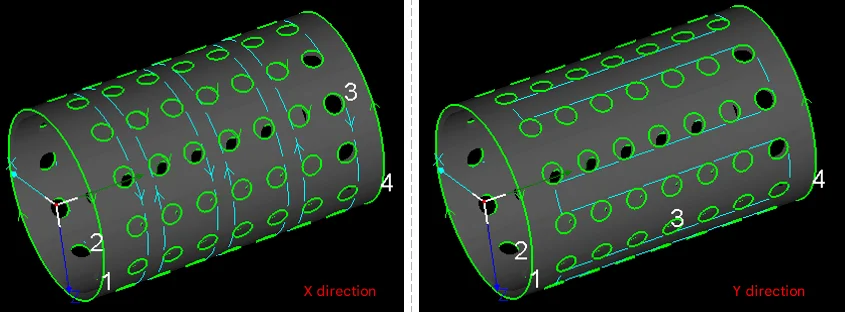
ソート方向: フライングカットの切断経路の方向によって、穴の切断順序が決まります。.
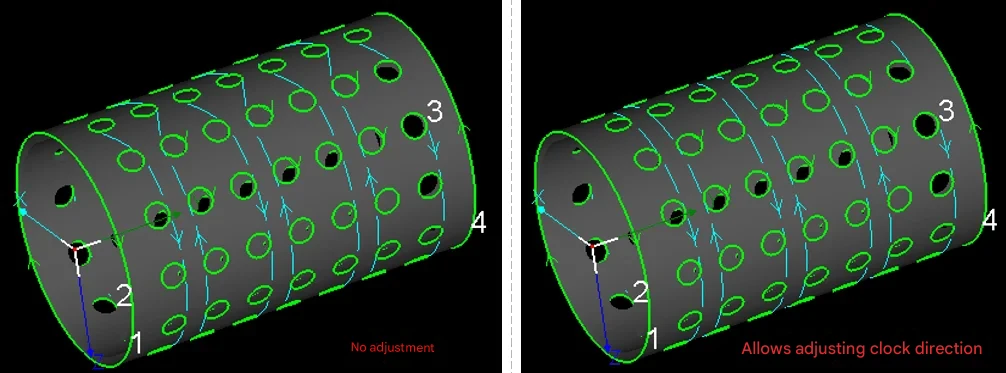
円弧時計回り方向の自動調整: 円形穴の開始位置と切断方向が異なる場合、生成されるフライングカットラインが乱雑になり、フライングカット軌道がスムーズでなくなる可能性があります。特別な要件がない限り、自動調整をチェックすることをお勧めします。チェック後、ソフトウェアはフライング軌道に従って各円形穴の切断方向を自動的に調整します。.
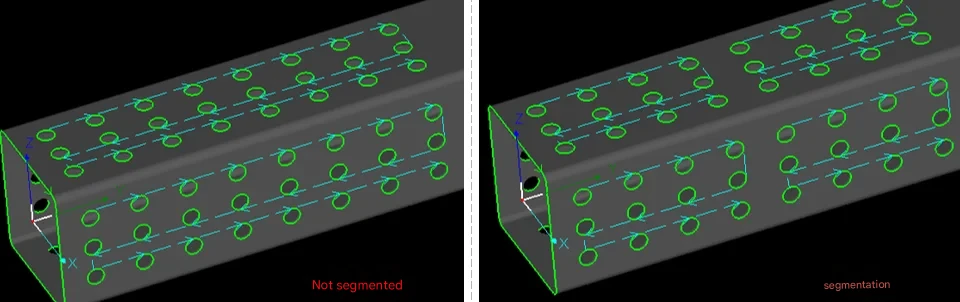
セグメント化フライングカット: 長い部品の場合、Y軸方向の長距離にわたるパイプ材料の頻繁な前後移動を避けるために、セグメント化フライングカットを使用することをお勧めします。.
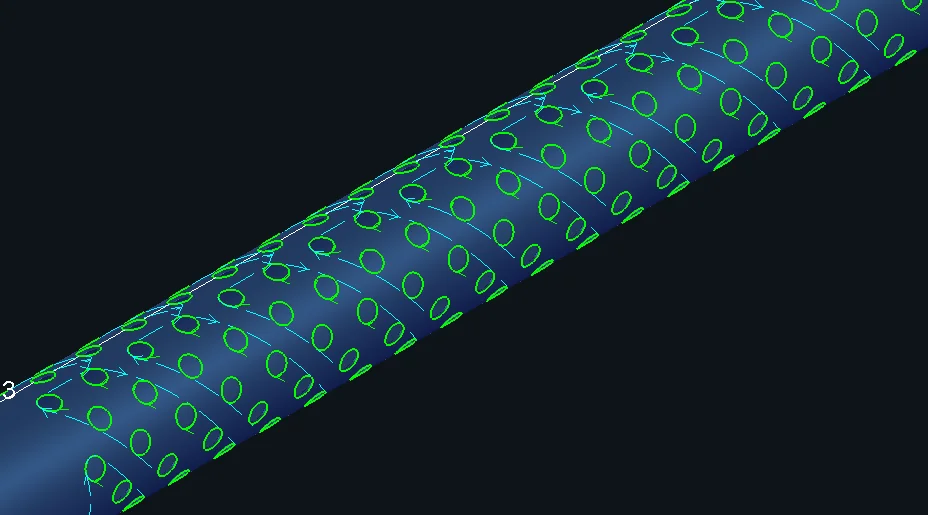
For。 千鳥配置 グラフィックのフライングカット設定:
(2)リニアフライングカット
角丸のない規則的に配置された長方形またはダイヤモンド穴の場合、丸パイプでも角パイプでも、, リニアフライングカット を使用する必要があります。.
許容距離偏差: 同じ直線上のセグメントをフライングカットラインで接続する場合、この直線からの距離偏差がこの設定値より小さいセグメントもこのフライングカット経路に計画されます。デフォルト値は20mmです。.

スムーズ接続の最大距離: ある列のフライングカットから別の列に切り替えるとき、この設定値より小さい旋回間隔はスムーズ接続を使用できます。(このパラメータは変更しないことをお勧めします)
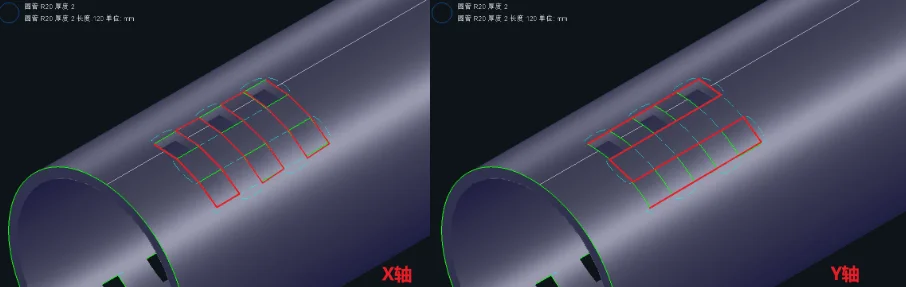
ソート:
フライングカットの場合、デフォルトでは最初にX方向に切断し、X方向の完了後にY方向に切断します。.
パイプ材料のクランプと移動プロセス中に、切断されていないパイプ材料がチャッククランプ内で持ち上がったり、落下していない破片がクランプ中にチャック内部に落ちてチャックに損傷を与え、機器の安全性と切断品質に影響を与える可能性があります。このとき、軌道のソート方向を自由に切り替えることができます。.
セグメント化フライングカット: 長い部品の場合、Y軸方向の長距離にわたるパイプ材料の頻繁な前後移動を避けるために、セグメント化フライングカットを使用することをお勧めします。.
(3)一筆書きフライングカット
一筆書きフライングカットは、テキストを除くすべての形状の穴に使用できます。一般的に、配列された楕円穴、角丸長方形穴などの切断に使用されます。.
アークフライングカットラインの最大半径: フライングカットラインの方向変更遷移に使用される最大半径で、推奨デフォルト値は3mmです。.
最大フライングライン長さ: The maximum flying line length supported between two adjacent graphics.
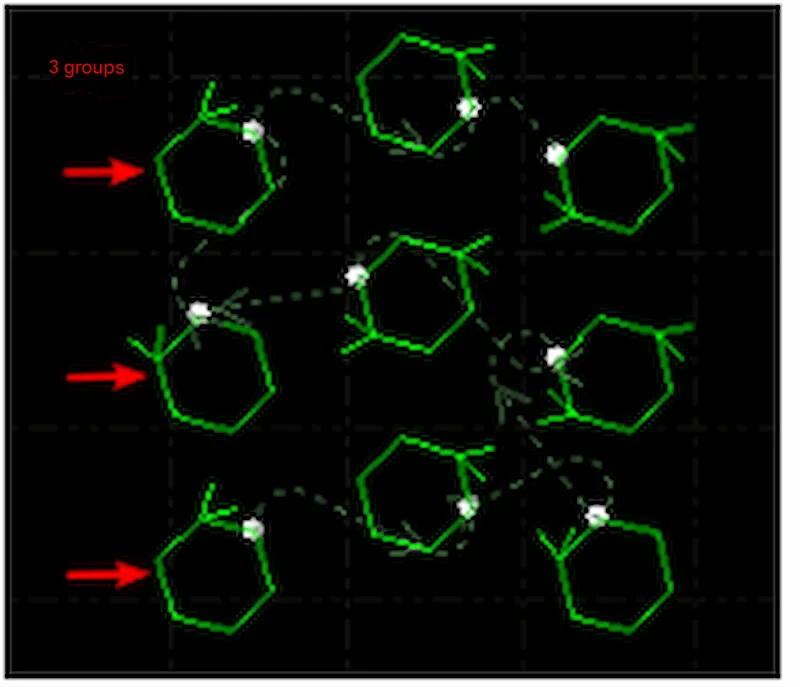
Serpentine sorting: Within the layout area, the cutting path presents a snake-like shape, as shown in the figure below:
Number of groups: The number of grid groups automatically divided for serpentine sorting.
4. What are the Advantages of Laser Fly Cutting?
(1) Significantly Save Time and Improve Work Efficiency
In traditional cutting mode, the cutting head needs to move from one location to another each time, with each movement consuming time. In fly cutting mode, the laser head flies directly to the target position and only starts working when actual cutting is needed. This means the entire cutting process no longer requires frequent stops and positioning, making cutting much faster than traditional methods, especially suitable for some long strip workpieces or high-volume processing requirements.
(2) Significantly Reduce Batch Production Costs
For single large parts, traditional cutting may be more efficient; but when involving more than 50 repeated graphics, fly cutting can save more than 60% of working hours. Longxin Laser uses intelligent nesting AI algorithms to achieve 92% steel utilization rate, significantly reducing batch production costs.
Fly cutting function is not suitable for all cutting tasks. To maximize the benefits of fly cutting function, detailed analysis of the workpiece material, thickness, and processing requirements is needed. For thicker metal materials, fly cutting mode may lead to unstable cutting quality, so it is necessary to choose whether to enable fly cutting function based on different situations. For thin plate materials or thin tubes, the effect of fly cutting is more obvious. It not only reduces wear caused by mechanical movement but also completes a large number of cutting tasks in a short time.
5. How to Use Laser Fly Cutting Function?
(1) Equipment and Material Preparation
Equipment Setup
- Verify that your laser cutting machine is equipped with fly cutting functionality
- Configure machine parameters based on material specifications:
- Adjust laser power according to material thickness
- Set appropriate cutting speed for the material type
- Calibrate the cutting head position
Material Setup
- Securely clamp the workpiece onto the cutting table
- Ensure proper material alignment and positioning
- Verify that the material surface is clean and free of debris
(2) Software Configuration and Programming
Step 1: Create or Import Graphics
- Open your cutting software (e.g., CypCut)
- Draw new graphics or import existing CAD files
- Focus on repetitive patterns such as circles, rectangles, or custom shapes
Step 2: Generate Pattern Arrays
- Select the base graphics that will be repeated
- Use the array function to create multiple copies:
- Set the number of rows and columns needed
- Define spacing between graphics (minimum 1mm to prevent collision)
- Preview the layout to ensure proper distribution
Step 3: Activate Fly Cutting Mode
- Locate the “Fly Cutting” option in the software interface (typically in the upper right corner)
- Select the appropriate fly cutting mode based on your graphics:
- アークフライングカット: For circular holes and curved patterns
- リニアフライングカット: For rectangular or square openings
- Racetrack Fly Cutting: For oval or elongated shapes
- One-Stroke Fly Cutting: For complex geometries requiring continuous paths
Step 4: Optimize Cutting Parameters
- Cutting Sequence: Define the order of operations (e.g., left-to-right, top-to-bottom)
- Micro-tab Settings: Configure small connection points (0.1-0.3mm) at start/end positions to prevent part movement during cutting
- Maximum Jump Distance: Set the maximum distance (1-5mm) the laser head can travel between cuts without interrupting the fly cutting sequence
- Precision Control: Adjust recognition deviation to 0.01mm accuracy to minimize path errors
(3) Execute Cutting Operation
Pre-Cutting Checklist
- Review the programmed cutting path and sequence
- Verify all safety systems are operational
- Ensure proper ventilation and fume extraction
During Cutting
- Monitor the cutting process continuously
- Watch for any irregularities in cut quality or machine behavior
- Be prepared to pause or stop the operation if issues arise
(4) Post-Cutting Quality Control
Immediate Inspection
- Examine cut edges for consistency and quality
- Check dimensional accuracy of finished parts
- Verify that all intended cuts were completed
Cleanup and Preparation
- Remove finished parts from the cutting table
- Clear away any cutting debris or slag
- Clean the worktable surface for the next operation
- Store completed parts according to quality standards
6. What are the Application Scenarios for Laser Fly Cutting?
Sheet Metal Dense Hole Processing
- Heat sinks/Filters: Efficiently cut large numbers of regularly arranged circular holes, square holes, or irregular holes, such as server chassis heat dissipation plates and air filter metal meshes. Fly cutting speed is more than 3 times faster than traditional methods.
- Architectural Decorative Panels: Hollow carving and railing grids on stainless steel/carbon steel thin plates (≤3mm). Complex patterns can be mass-produced through linear or arc fly cutting.
Pipe and Structural Component Processing
- Automotive Exhaust Pipes/Agricultural Machine Brackets: High-speed hole opening or cutting connection parts on round pipes and square pipes. Bond Laser T-series five-axis pipe cutting machines support fully automatic fly cutting for φ20-600mm pipes.
- Elevator Panels/Control Cabinets: Button holes and wire groove opening groups on thin steel plates, using one-stroke fly cutting mode to reduce empty movement paths.
Advertising Signs and Craft Gifts
- Metal Nameplates/Logos: Fine text hollowing on stainless steel or brass thin plates, such as corporate logos and artistic letters.
- Cultural and Creative Products: Laser hollow patterns on greeting cards and bookmarks (such as flowers, geometric patterns), three-dimensional assembly models of acrylic materials.
Consumer Electronics and Home Appliances
- Electrical Enclosure Heat Dissipation Holes: Group circular hole fly cutting on air conditioning panels and power box covers, requiring hole position accuracy of ±0.1mm.
- 3C Components: Mobile phone middle plate positioning holes, headphone metal mesh covers. Han’s Laser ultrafast laser technology achieves micron-level cutting.
7. Longxin Laser Fly Cutting Solutions
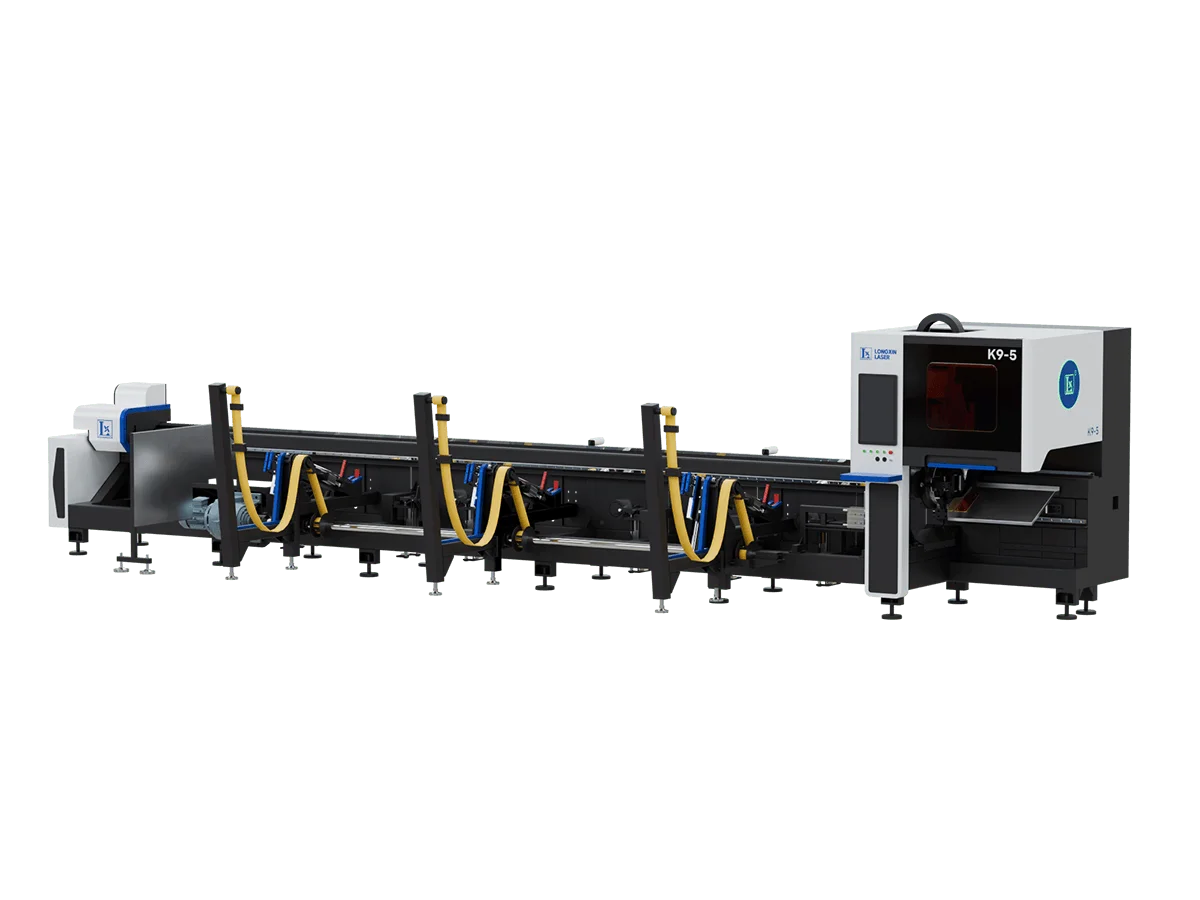
Longxin Laser offers advanced laser tube cutting machines equipped with cutting-edge fly cutting technology. Our machines feature high-performance capabilities with maximum acceleration up to 2.0G, ensuring rapid and precise processing for demanding industrial applications.